


A recycled-plastic line can produce pellets that look acceptable while volatile contamination is already moving through the degassing system. Odorous compounds, residual products from the material’s previous use and processing by-products may change from one feed batch to the next. If the plant waits for finished-pellet testing or complaints, it loses the chance to correct the process while the material is still in the extruder.
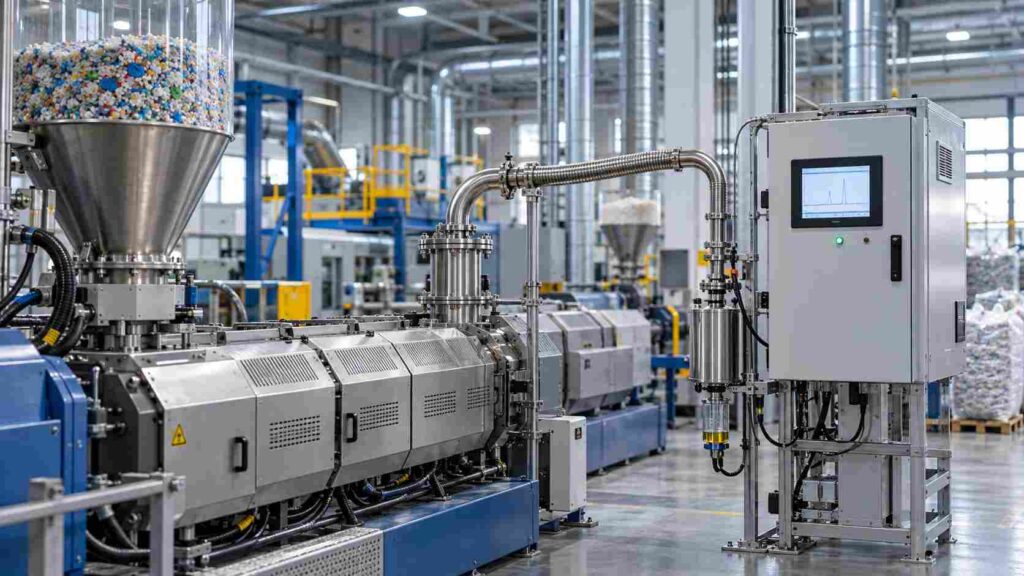
Plastic extruder degassing gas monitoring should combine a continuous indication of volatile loading with periodic compound-specific analysis and process data. The sampling system must preserve representative compounds across the expected range of volatility, polarity, temperature and pressure rather than relying on a universal VOC sensor or a single cold trap.
The most important engineering decision is how the gas is transferred from the process to the measurement. A detector can be sensitive and properly calibrated yet still deliver a biased result if water, oil or organic vapour condenses before analysis, or if the sample point does not represent the material being processed.
Why Does Degassing Gas Matter to Recycled-Polymer Quality?
Finished-pellet tests describe the material after the opportunity for correction has largely passed. A time-resolved gas signal can reveal when a feed change, poor drying or unstable vacuum begins to release a different volatile mixture.
The vacuum degassing port provides access to compounds leaving the polymer melt. In post-consumer material, the mixture can include residues from earlier contents, washing chemicals, degradation products, additives and reaction products formed during processing. Recycled polymer VOCs are therefore not one stable gas family.
A 2026 study of recycled polypropylene detected more than one hundred volatile compounds across condensate and adsorbent samples, including many odor-active components. That finding does not mean every plant must measure the same list. It shows why initial screening is needed before a small set of routine indicators is selected.
Which Compounds Should Be Screened?
Monitoring only a total signal can show that something changed but not whether the change matters for odour, product quality or treatment. Measuring every identified compound continuously, however, is rarely practical.
| Measurement layer | Possible targets | Use |
| Total trend | Total hydrocarbons or total VOC response | Detect rapid changes and compare production periods |
| Compound groups | Aldehydes, ketones, alcohols, acids and hydrocarbons | Link patterns to odour, oxidation or contamination |
| Specific markers | Plant-selected compounds | Track a feedstock, washing or product-quality issue |
| Process context | Water vapour, CO₂, O₂, pressure and flow | Interpret dilution, drying and vacuum performance |
| Periodic unknown screening | Broad chromatographic or mass-spectral scan | Update the permanent target list |
Gas-phase contaminant screening should begin with representative raw-material classes and operating modes. The resulting list can then be prioritised by odour relevance, product specification, safety and environmental requirements. A compound that is important for one recycled-polymer stream may be irrelevant to another.
At ESEGAS, we would define the routine indicator set only after the plant has mapped its feed variability and the analytical objective. A VOC trend channel can support process decisions, but compound identity and trace-level confirmation may require chromatography or laboratory analysis.
Why Is Sampling at the Degassing Port Difficult?
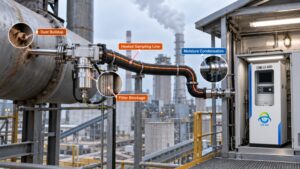
The gas at the process connection may be hot, wet, under deep vacuum and rich in condensable material. Bringing it to an analyzer at ambient pressure changes the equilibrium, so the sample can separate before it is measured.
Condensate fractionation occurs because different compounds have different volatility, polarity and water solubility. A cold trap may collect heavier or water-soluble material while a sorbent retains another fraction. The 2026 polypropylene study found that condensate and adsorbent samples did not represent the same mixture, which is a warning against treating one fraction as the complete gas.
Sorbent-tube sampling can extend coverage, but loading, water interference and breakthrough must be controlled. Very long collection periods can overload the tube or blur a short process event. An automated sampling train should therefore control timing, valve switching, condensation and purge cycles as carefully as the analytical detector.
- Measure pressure and temperature at the process connection.
- Use inert, low-volume wetted parts and minimise uncontrolled cold surfaces.
- Define which condensed and non-condensed fractions are included in the result.
- Provide a controlled path for condensate without allowing it to re-evaporate into a later sample.
- Test recovery with compounds that represent the volatility and polarity range of interest.
Where Should Measurements Be Taken?
A result at the final exhaust may support an emissions question but cannot show whether the polymer, vacuum system or condenser caused the change. A result directly at the process can support quality control but may not represent what reaches the atmosphere.
| Point | Main question |
| Degassing port | What leaves the polymer melt? |
| Condenser inlet/outlet | Which fraction is captured and which passes through? |
| Vacuum-pump discharge | What mixture enters ventilation or treatment? |
| Treatment outlet | What remains after carbon, oxidation or another control stage? |
| Finished pellet | Does the gas trend correspond to final material quality? |
Useful locations include the extruder degassing dome or line, before and after a condenser, the vacuum-pump discharge and the final treatment outlet. Extruder vent monitoring at more than one location allows the plant to distinguish material release from capture or treatment performance.
Each point needs its own range and sample design. The raw line may require brief, controlled collection under vacuum; the pump outlet may be at a more convenient pressure but can contain pump-related contamination; the final exhaust may be diluted by ventilation air.
Which Analytical Methods Are Suitable?
A fast total-VOC instrument and a detailed laboratory chromatogram answer different questions. Selecting one as a universal replacement for the other can either hide compound identity or make routine control too slow.
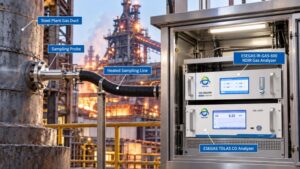
FID or PID instruments can provide a rapid trend when their response factors and sample compatibility are understood. FTIR may measure configured infrared-active components, particularly when water and cross-interference are addressed. Thermal-desorption GC-MS or GC-MS/olfactometry can identify a much wider range of compounds and connect chemical peaks with odour, but it is generally a periodic or at-line method.
An integrated system may use a continuous channel for rapid change detection and trigger an automated or manual speciation sample when the signal crosses a plant-defined condition. Recycled-plastic odour control then uses both the timing of the event and the compound pattern rather than an isolated total value.
- Use total-response instruments for stable, high-frequency trending.
- Use selected optical channels where a known compound group can be validated.
- Use sorbent tubes, canisters or condensate collection for laboratory identification.
- Use GC-MS/O when sensory relevance must be connected to chemical composition.
- Repeat broad screening when feedstock or washing and deodorisation steps change.
How Can Data Support Process and Odour Control?
A gas trend without material and machine context may identify a change without showing how to correct it. Linking the measurement to the right production batch turns it into actionable process information.
The data system should align gas readings with feedstock source, batch, moisture, barrel temperatures, screw speed, throughput, vacuum pressure, vent flow and condenser status. It should also record cleaning, material transitions and downtime because residues from a previous batch can appear during the next run.
Operators can compare the volatile pattern with pellet odour, colour, melt properties and laboratory quality results. Over time, this can support feed segregation, drying changes, vacuum optimisation or a decision to route a batch through additional deodorisation. It should not be used to make food-contact or safety claims without the appropriate product testing.
Why Must Process, Workplace and Stack Monitoring Remain Separate?
One detector cannot simultaneously represent the polymer melt, a worker’s breathing zone and a regulated exhaust. These locations have different ranges, time scales and legal purposes.
Process measurements support material quality and machine control. Workplace detectors or industrial-hygiene sampling evaluate potential exposure near equipment. Stack or ventilation monitoring evaluates the controlled release. The same compound may appear in all three layers, but the sampling location and performance requirements are not interchangeable.
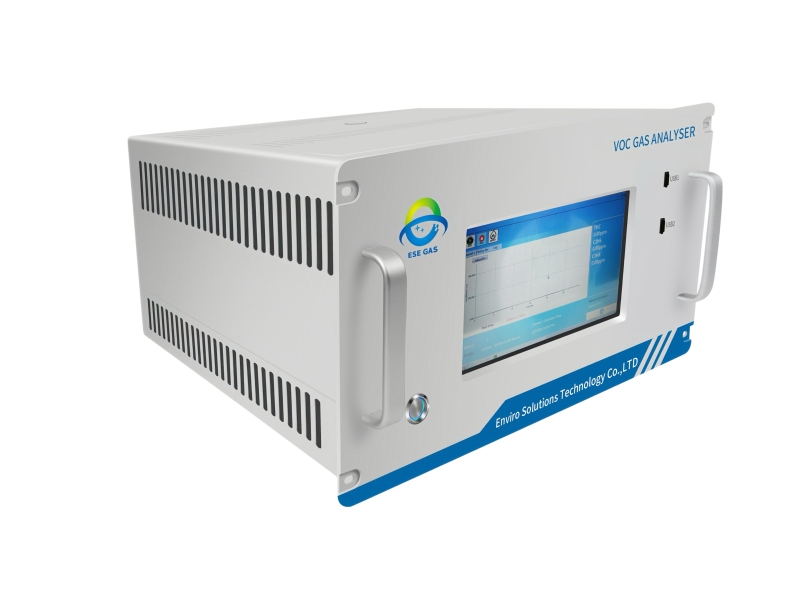
At ESEGAS, we recommend defining the decision attached to each result before selecting the instrument. A process VOC analyzer can be useful for extruder control, while a permit measurement may require a specified reference method and an independent safety detector may need its own alarm logic.
How Should Measurement Quality Be Verified?
A stable output can be produced by a partially blocked line or a saturated adsorbent. Quality controls must reveal whether the sample still represents the process as feed composition and condensate loading change.
Commissioning should include blanks, recovery tests, breakthrough checks, response-time measurement and comparison between collected fractions. The plant should document how condensate is handled, how often lines and traps are cleaned, and how memory from one batch is excluded from the next.
We also recommend retaining raw chromatograms or spectra when available. If an odour or product-quality issue appears later, the original data can be re-examined for compounds that were not part of the first routine list.
- Challenge the complete path, not only the detector.
- Verify sampling time and valve timing under vacuum.
- Check for sorbent breakthrough and water interference.
- Use field blanks and carryover tests between feed batches.
- Synchronise gas, process and product-quality timestamps.
Plastic extruder degassing gas monitoring is fundamentally a sampling problem before it is an analyzer problem. At ESEGAS, we recommend combining a validated high-frequency VOC trend with periodic speciation, controlled handling of condensate and adsorbates, and batch-linked process data. This layered design helps recyclers recognise feed changes, improve odour control and evaluate degassing performance while keeping process information, workplace protection and formal emissions monitoring in their proper roles.